
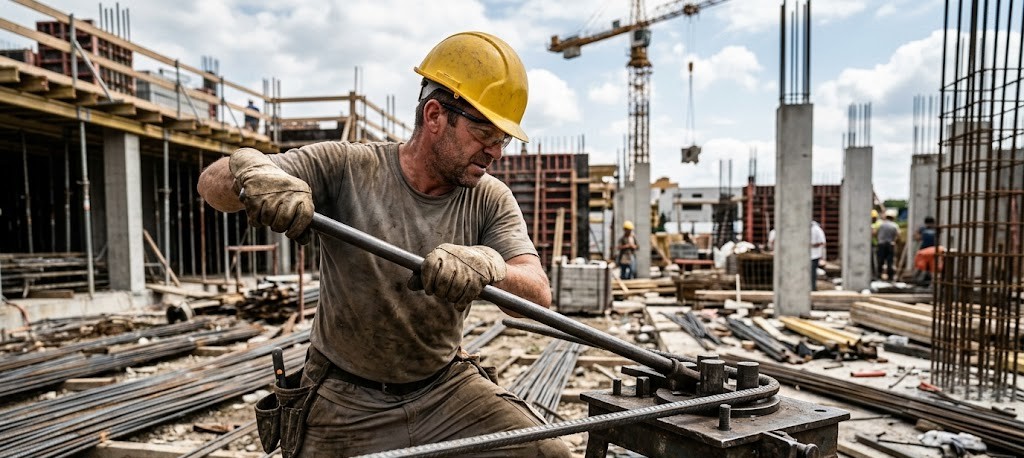
The most common mistakes made when processing rebar center on using a machine with the wrong capacity, inaccurate measurements, unsuitable bending settings, irregular material flow and neglected machine maintenance. These mistakes can affect not only the quality of the prepared reinforcement but also labor time, material use and production organization on the construction site.
The main risk areas are choosing a cutting or bending machine unsuited to the bar diameter, leaving measurement checks until after processing, pushing the machine beyond its operating capacity and positioning cutting and bending stations without a plan. Göçmenler Group's product portfolio includes equipment groups for different working needs, such as rebar cutting, bending, mesh bending and combined cutting-bending machines.
Choosing a machine that does not match the bar diameter and daily processing volume is one of the main mistakes encountered on site. Evaluating a machine's capacity based only on motor power is not enough. The properties of the bar to be cut or bent, the number of bars to be processed at the same time and the workload should be evaluated together.
Göçmenler Group's bar bending product group includes models for different capacities: the AG 24, AG 26, AG 32, AG 34, AG 36, AG 55 and AG 60. The cutting machine group also offers various capacity options in the TG and TM series.
“The right machine capacity ensures not only that the reinforcement can be processed, but that the operation continues in an orderly and sustainable way.”
In practice, constantly pushing capacity limits can reduce production pace and increase the load on the equipment. The solution is to determine the bar diameters to be used and the estimated daily processing volume before the project starts and select the appropriate equipment.
Reinforcement cut to the wrong length usually affects subsequent operations directly as well. If a measurement error is noticed at the bending or installation stage, the same part may need to be prepared again, slowing down the material flow.
For this reason, it is important to organize cut lists before cutting, group similar lengths and check the first piece. A quick measurement check before moving on to serial production can prevent the same error from being repeated across many bars.
| Common Mistake | Possible Consequence | Applicable Solution |
| Wrong capacity selection | Slow operation, equipment strain | Select the machine by bar diameter and workload |
| Incorrect cutting dimension | Material waste, reprocessing | Measure the first piece before serial cutting |
| Incorrect bending setting | Angle and shape deviations | Check settings before production |
| Unplanned material flow | More waiting and handling | Plan the cutting and bending line together |
| Delayed maintenance | Unplanned downtime | Add periodic checks to the work schedule |
“In serial production, a small measurement error can turn into a significant loss of work and material when it is repeated.”
The main mistake in bending is keeping the same machine setting for different reinforcement needs. When the diameter of the bar to be bent, the required shape and the number of operations change, the equipment settings must be adjusted accordingly.
Göçmenler Group's bar bending machines are divided into different capacity groups, and the technical specifications of the products are stated according to the number and diameter of bars that can be processed. For example, for the compact SMALL 26 model, capacity values are given separately according to the number of bars and material strength.
“Consistent bending quality depends on the right processing settings as much as on the right machine.”
In practice, it is useful to prepare a few test pieces before serial bending. Moving on to serial work after the angle, shape and dimensions have been verified reduces the risk of many parts being prepared incorrectly. Setting changes must be kept under control, especially on sites where different diameters are processed within the same shift.
One of the main causes of lost time in rebar processing is positioning the cutting and bending stations without considering material flow. Carrying cut bars over long distances or piling them up before bending increases operator movement and can disrupt production.
Because Göçmenler Group's product portfolio includes diesel combined cutting-bending machines in addition to separate cutting and bending machines, equipment can be planned according to different construction site layouts.
“In an efficient rebar preparation area, the goal is not just to position the machines but to shorten the path the material follows.”
The input point for the bars to be cut, the cutting section, the bending station and the output area for finished parts should be planned as a whole. Such a layout reduces unnecessary handling while supporting more controlled use of the working area.
When maintenance is addressed only after a breakdown, the risk of unplanned downtime for rebar processing machines increases. Daily inspection, cleaning and planned maintenance play an important role in keeping the machine running properly.
Göçmenler Group states that it provides technical service and spare parts services in addition to rebar cutting and bending machines. For this reason, when selecting equipment, the post-purchase service and maintenance process should be evaluated as well as the machine's technical capacity.
“Planned time set aside for maintenance is easier to manage than the time lost to an unexpected machine stoppage.”
Operators checking the general condition of the machine before starting work, keeping the working area tidy and paying attention to unusual noises or behavior make early intervention easier.
Most mistakes in rebar processing can be reduced with an orderly control system set up before the machine is used. An effective workflow can follow this sequence:
The most common mistakes made when processing rebar mostly stem from a lack of control over equipment capacity, measurement, settings and working setup. Correctly matching Göçmenler Group's machine options for different cutting and bending needs with project requirements helps create a more orderly, controlled and efficient reinforcement preparation process.